Hey everyone, it’s Jake here from your go-to welding wire winding machinery supplier—today we’re getting real about something that trips up even our most regular clients: bearing replacement in those winding lines. I’ve lost count of how many times I’ve gotten a frantic 7AM call from a shop foreman because their line went down mid-batch, all because a bearing seized up. The good news? This fix isn’t nearly as scary as it sounds—if you know what you’re doing, you’ll be back up and running faster than you can reload a spool of wire. Let’s break this down step by step, no fancy jargon, just stuff we actually use in our service bay every day. Welding Wire Winding Machinery
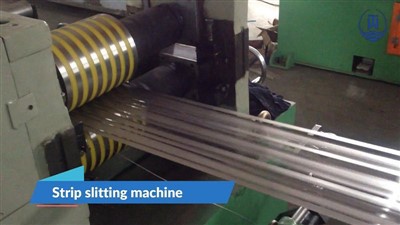
First off, why does this even matter? Welding wire winding machinery runs nonstop, right? Pulling 12,000-foot spools of solid wire through at 500 feet a minute? That generates heat, vibration, and wear like crazy. The bearings are the unsung heroes here—they hold the winding shaft steady, keep the tension consistent, and if they crap out, you’re not just replacing a part. You might mess up a whole batch of wire, damage the guide rollers, or even throw the whole shaft out of alignment. I see this mistake all the time: guys just yank out the old bearing and jam in a new one, no prep, no checks, and it’s garbage in a week. Don’t be that guy.
First step: Prep like your line depends on it (it does). Let’s talk safety first—turn that power off. Unplug it, lock the breaker, tape a sign on it so no one hits the wrong switch while you’re kneeling under the machine. I learned this the hard way once when a new intern flipped the breaker back on while I was reaching into the winding head—scared the crap out of me, and I had a band-aid on my finger for a week. No shortcuts here. Next, gather your tools: a bearing puller (the two-jaw kind, not that cheapy three-jaw that slips), a mallet (rubber, not steel—you’ll ding the shaft), a small pry bar, some isopropyl alcohol, a lint-free cloth, and of course, your new bearing. Wait—hold up, don’t grab just any bearing. Check your manual, take the old one with you to order, and get a premium sealed bearing, not a cheap Amazon knockoff. I’ve had clients save $10 on a bearing only to replace it three months later—total waste of time. Also, clean the area around the bearing housing before you touch anything. If you’ve got metal shavings or dust in there, that’s gonna get packed into the new bearing and kill it fast. Blast it with compressed air if you have it, or wipe it down with alcohol till the cloth comes up totally clean.
Next, get the old bearing out. This is where people mess up. If you just pry at it, you’ll bend the housing or score the shaft, and that’s a way bigger repair. Slide the puller jaws under the outer edge of the bearing, not the inner race. Tighten the puller bolt, then give the center of it a gentle tap with the mallet. If it won’t budge, don’t crank the puller—tap the puller’s body a few times to break the seal between the bearing and the housing. I keep a can of penetrating oil in my service truck too—spray a little around the edge, let it sit 10 minutes, then go back to the puller. If the bearing’s totally seized, you might have to use a chisel to score the outer race (just don’t hit the shaft), but nine times out of ten, the puller works. Once it’s out, inspect the shaft and housing. Score marks on the shaft? Minor ones can be buffed out with 320-grit sandpaper, but if it’s deep, you’ll need to replace the shaft. Housing grooves? Same thing—minor ones get cleaned, deep ones need a housing sleeve. This is why we stress inspection, not just swap.
Now, the new bearing part. Here’s another common mistake: people either heat the bearing too hot, or just jam it in with a mallet. If you hit the inner race, you can damage the ball bearings inside, and if you overheat it, you’ll mess with the bearing’s heat treatment. The right way: heat the bearing evenly, to about 200-250°F—warm enough that you can touch it with your bare hand without burning. You can do this with an oven (lay it on a wire rack, no direct contact with the pan) or a heat gun on low, moving it around so you don’t melt any seals. Never use a torch—too easy to get it too hot. Once it’s warm, slide it onto the shaft, lined up so the sealed side faces the load (meaning, the side that’s facing the inside of the machinery, away from dust). Then, use the old bearing as a drift—set the old bearing’s inner race against the new one’s inner race, and tap gently with the mallet to seat it evenly. Don’t hit the outer race, and don’t hammer it hard—if it won’t slide on, heat it a little more, don’t force it. Now, slide it all the way into the housing, make sure it’s flush. Wipe away any extra heat transfer stuff, let it cool for 15 minutes before turning anything on.
Wait, did I miss a step? Yeah—lube. Most new bearings come pre-lubed, but if yours doesn’t, use the right grease. Not regular wheel bearing grease, not lithium grease—get the high-temperature, food-grade grease if you’re doing galvanized or solid wire, or the high-load industrial grease for hard-drawn wire. Too much grease is as bad as too little—pack the bearing cavity about ⅔ full, wipe off the excess so it doesn’t get flung onto your wire. I always have a tube of this stuff in my service van—way better than the dinky tube that comes with most DIY kits.
Once everything’s seated, do a quick pre-start check. Spin the winding shaft by hand. Does it spin smooth, no gritty spots, no tight areas? If it sticks, you probably didn’t seat the bearing right, or there’s a burr on the shaft. If it feels smooth, put everything back together. Tighten the mounting bolts to the torque spec in your manual—don’t over-tighten, that will warp the housing and mess up the bearing. Once it’s all buttoned up, test run it on low speed first. Let it run for 5 minutes, check for noise, vibration, or heat. If it’s running quiet, smooth, and not overheating, you’re good to go.
Now, let’s talk maintenance so you don’t have to do this again next month. We see clients who change oil in their cars every 3,000 miles but skip lubricating their winding machinery bearings every 6 months, and wonder why they’re failing. For welding wire winding lines, check the bearings every 500 hours of operation, relube them every 1,000, and replace them every 2-3 years—more if you’re running 24/7. Also, keep the machine clean—metal shavings are the #1 cause of bearing wear. A quick wipe down after every shift will save you hours of downtime.
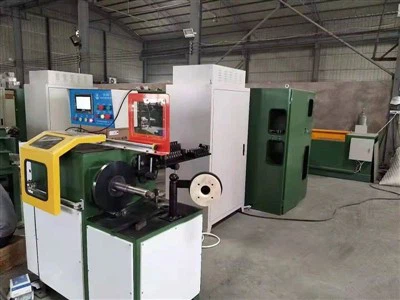
Look, we get it—your welding wire winding machinery is your livelihood. If it’s down, you’re not making money. That’s why we built our service team to help with this exact stuff. We’ve been selling and servicing winding lines for over a decade, so we know every trick, every mistake, every part that works (and the ones that don’t). If you’re not sure which bearing to get, or if you run into a snag mid-replacement, or you just want a pro to come out and do it for you, hit us up. We don’t do pushy sales, we do honest advice for people who need to keep their lines running.
Welding Wire Winding Machinery Don’t waste time messing around with bad parts or wrong techniques. A proper bearing replacement will keep your line running smooth for months, no hiccups. Remember: prep is key, tools matter, and don’t skip the inspection. If you follow this, you’ll be back to winding wire faster, and you won’t have to deal with that 7AM panic call next time.
References
- American Welding Society. (2019). Maintenance Guidelines for Industrial Welding Wire Handling Equipment. AWS D1.10 Standard.
- SKF Group. (2021). Bearing Installation and Replacement Handbook for Industrial Power Transmission Equipment. SKF Technical Publications.
- Machinery Lubrication Magazine. (2020). Common Bearing Failure Causes in High-Speed Winding Applications. National Lubricating Grease Institute.
Three Water Machinery Co., Ltd.
Three Water Machinery Co., Ltd. is one of the most reliable manufacturers and suppliers of welding wire winding machinery in China. With abundant experience, we warmly welcome you to buy advanced equipment for sale here and get quotation from our factory. Contact us for more details.
Address: No.15, Jiaye Road, Liuanzhuang Industrial Park, Beichen District, Tianjin, China
E-mail: sales@eqet.com
WebSite: https://www.eqet.com/
